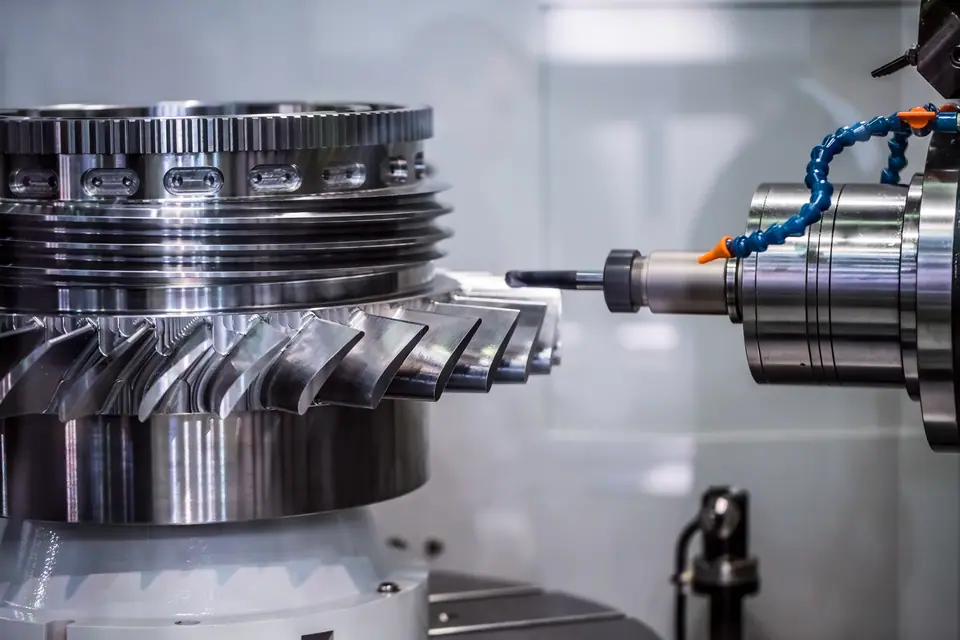
CNC milling
Pockets, profiles, holes, threads and 3D surfaces on vertical machining centres. Ideal for housings, brackets, plates, fixtures and complex prismatic parts.
CNC machining service
Precision milled and turned parts in metals and engineering plastics — from a single prototype to low- and medium-volume production. Every quote is reviewed by an engineer, and every part is inspected before it ships.
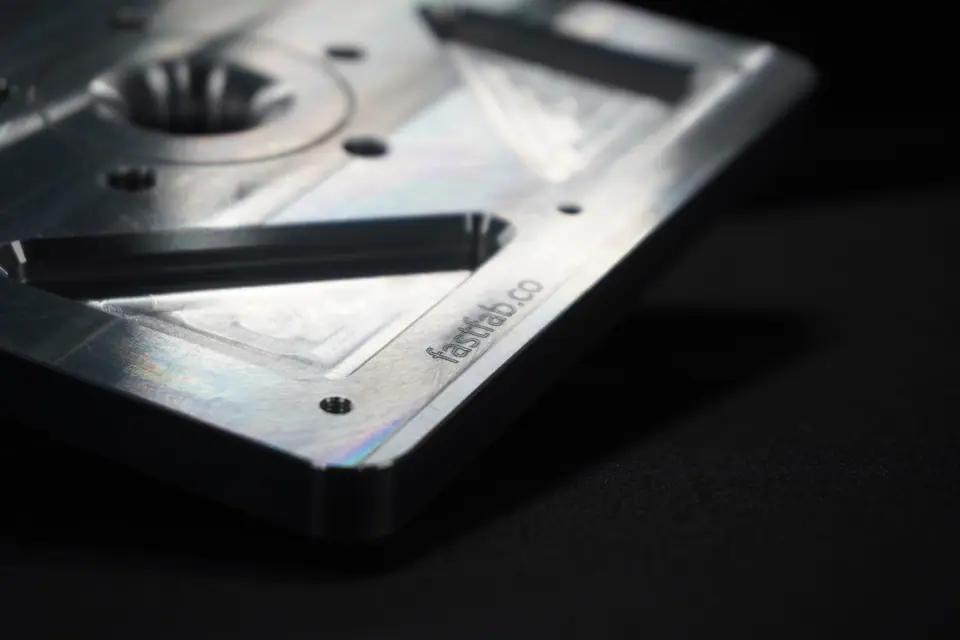
FastFab in production
We take a comprehensive approach to every project, developing reliable, scalable solutions that support long-term partnerships. Whether the goal is shorter lead times, a design optimised for manufacturability, lower cost or tight tolerances with a superior finish, we tailor the process to your requirements.
Our CAD/CAM workflow carries your 3D model straight to the machine, keeping accuracy and repeatability high from the first part to the last.
| Processes | 3-axis+ CNC milling on vertical machining centres CNC turning for shafts, fittings and round parts |
|---|---|
| Tolerances | Down to ±0.05 mm on critical features General tolerances to ISO 2768-m unless specified |
| Quantities | One-off prototypes to low- and medium-volume production |
| Metals | Aluminium 6061, 6082, 7075, 2024, 5083 · Steel S235JR, S355J2, C45, 42CrMo4, 11SMnPb30 · Stainless 303, 304/304L, 316L, 17-4 PH |
| Plastics | POM-C, PA6/PA66, PE-UHMW, PE-HD, PP, PTFE, PET-P, PC, PMMA, PEEK |
| Finishes | As machined, sandblasted, anodised (aluminium), coated |
| Quality | Inspection against your drawing; material certificates and inspection reports on request |
| Files | STEP / IGES 3D model + PDF drawing (tolerances, threads, surface finish) |
Processes
Pockets, profiles, holes, threads and 3D surfaces on vertical machining centres. Ideal for housings, brackets, plates, fixtures and complex prismatic parts.
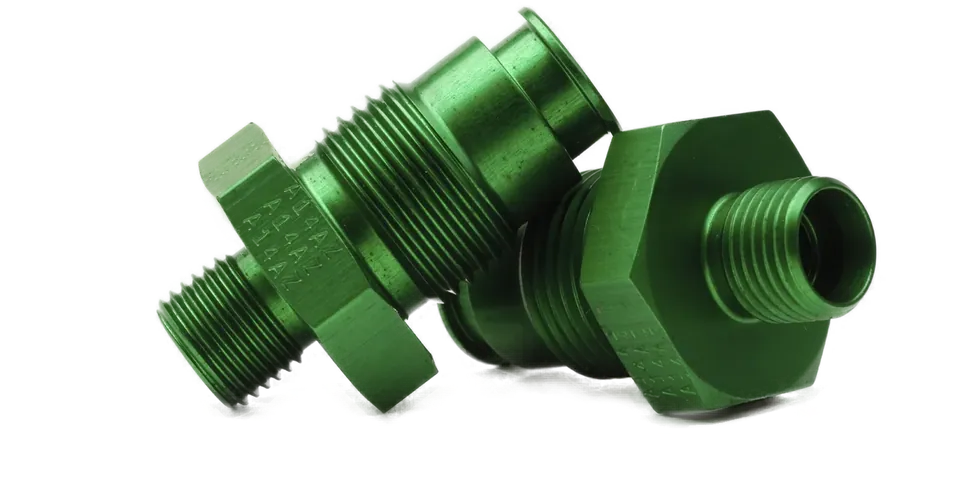
Round parts such as shafts, bushings, spacers and threaded fittings, turned to tight concentricity and finished to your specification.
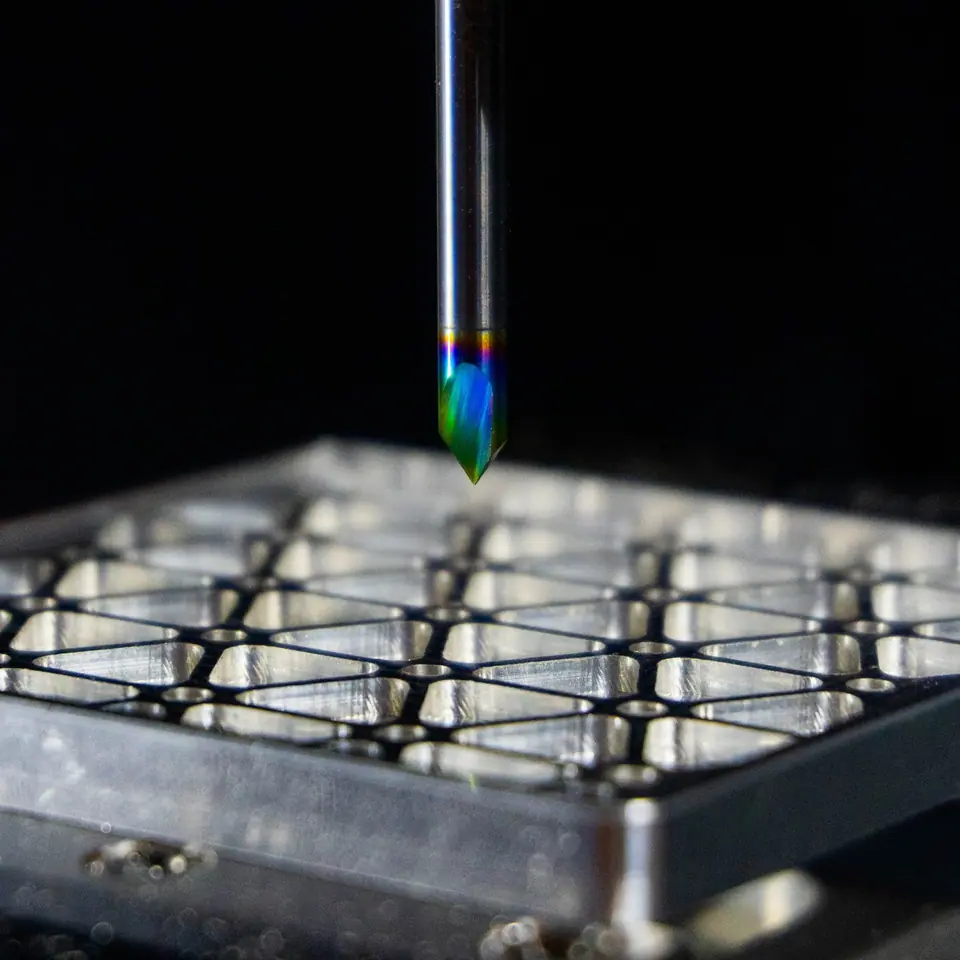
Deburring, sandblasting, anodising and coating, so parts arrive ready for assembly — not just ready for another supplier.
Gallery
DFM
End mills are round — use R2–R3 corner radii, or dogbones where square corners must mate.
Aim for a depth of 3–4× the tool diameter: a 3 mm cutter reaches about 10–12 mm.
Apply tight tolerances to fit-critical features only and leave the rest to general tolerances (ISO 2768-m).
Standard drill and tap sizes mean fewer tool changes and faster machining.
Applications
FAQ
We machine critical features to tolerances down to ±0.05 mm. Dimensions without a tolerance follow ISO 2768-m general tolerances. Mark critical tolerances on your drawing and our engineers will confirm feasibility in the quote.
Machining cost depends on setups, tooling, tolerances and material, so every CNC quote is reviewed by an engineer. Send your files through the quote page or the contact form and we’ll reply with a detailed quotation, lead time and DFM feedback.
Aluminium (6061, 6082, 7075, 2024, 5083), steels (S235JR, S355J2, C45, 42CrMo4, free-machining 11SMnPb30), stainless steels (303, 304/304L, 316L, 17-4 PH) and engineering plastics such as POM-C, PA, PE-UHMW, PTFE and PEEK. See the materials page for details.
Yes. Material certificates and inspection reports are available on request — let us know when you place your order.
Yes. We offer anodising for aluminium, as well as sandblasting and coating.
Upload STEP, STL or 3MF files for an instant 3D printing estimate, or send your CNC drawings for an engineer-reviewed quote. NDA available on request.